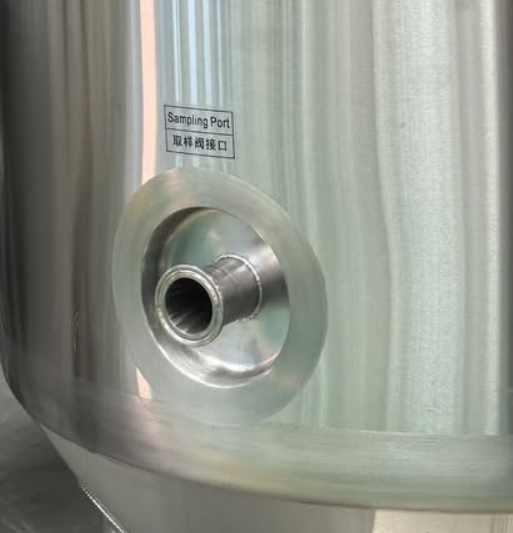
A sampling valve may look like a tiny, insignificant fitting in a complete craft brewing system. Some brewers even treat it as an optional extra and allocate little budget to this small component. However, for fermenters, bright beer tanks and mash tuns, the sampling valve serves as the critical connection between brewers and the wort or beer inside the tank. A hygienic and reliable sampling valve is indispensable for process control, flavour evaluation and risk detection throughout the whole brewing cycle.
Testing samples is required at every stage of brewing. After mashing, samples are taken to measure the original gravity of wort and confirm whether starch conversion reaches the target. During fermentation, regular sampling tracks specific gravity, diacetyl level and pH value to judge fermentation progress. In cold storage, brewers check clarity of the beer and monitor maturation.
A final flavour check is also necessary before packaging. Without dedicated sampling valves, operators would have to open manholes or disconnect pipe joints to collect samples. This method is not only cumbersome and time-consuming, but also introduces major risks. Opening the tank exposes the liquid to air, which easily triggers oxidation and creates stale, cardboard-like off-flavours that ruin the delicate beer profile. Harmful microbes from the surrounding air can also enter the tank and cause souring of the whole batch.
High-quality sampling valves for beer production are engineered with sealing performance and sanitation as top priorities. Only a small volume of liquid is released during sampling, while the tank remains sealed. Internal pressure and CO₂ atmosphere stay stable, limiting oxygen intake effectively. Most brewing-grade sampling valves are compatible with CIP cleaning. Cleaning fluid flows through the valve cavity to remove residual wort or beer, preventing buildup inside gaps. This avoids dead zones where contaminants can grow quietly and pollute subsequent batches.
Sampling valves help brewers spot abnormalities at an early stage. Continuous sampling and testing can capture warning signs such as slow fermentation, stuck diacetyl reduction or unexpected haze. Temperature and pressure settings can be adjusted promptly before issues escalate. Without a dependable sampling point, defects may only be discovered at filling time, which often means the entire tank of beer is wasted and brings heavy economic losses for small craft breweries.
Tanks have different sampling requirements. Fermenters work under pressure, so pressure-resistant sampling valves are required. Finished beer in bright beer tanks is extremely sensitive to oxygen, so low-oxygen designs are preferred. Valves fitted on mash tuns must withstand high-temperature wort. Low-grade sampling valves commonly have many hidden crevices, poor cleanability, leak-prone seals and stiff operation. Over time, these faults continuously contaminate beer or let air in during sampling. Many unexplained flavour problems in breweries can be traced back to improperly selected or poor-quality sampling valves.
Besides lab testing, sampling valves support direct flavour tasting. Brewers can take small portions to assess aroma and taste, which cannot be fully replaced by instrument readings. Controlled small-volume sampling also cuts down product loss, as there is no need to drain large amounts of beer.
Even the best sampling valve cannot work reliably without proper care. A quick rinse after each sampling and regular sanitisation alongside tank CIP cycles are necessary. Sealing gaskets should be inspected periodically for ageing. Without routine maintenance, even premium valves can turn into contamination sources.
To sum up, the sampling valve acts as a monitoring window for brewers. It enables sealed sampling, minimises oxygen pickup and microbial ingress, supports ongoing tracking of gravity, fermentation status and flavour, and helps prevent costly production failures. Though compact, this small fitting is vital for consistent beer quality and lower rejection risk.